Information and training
Provide current operating, maintenance and safety information for Bottle Checkweighers, plus settings, software backups, training and any outstanding actions.
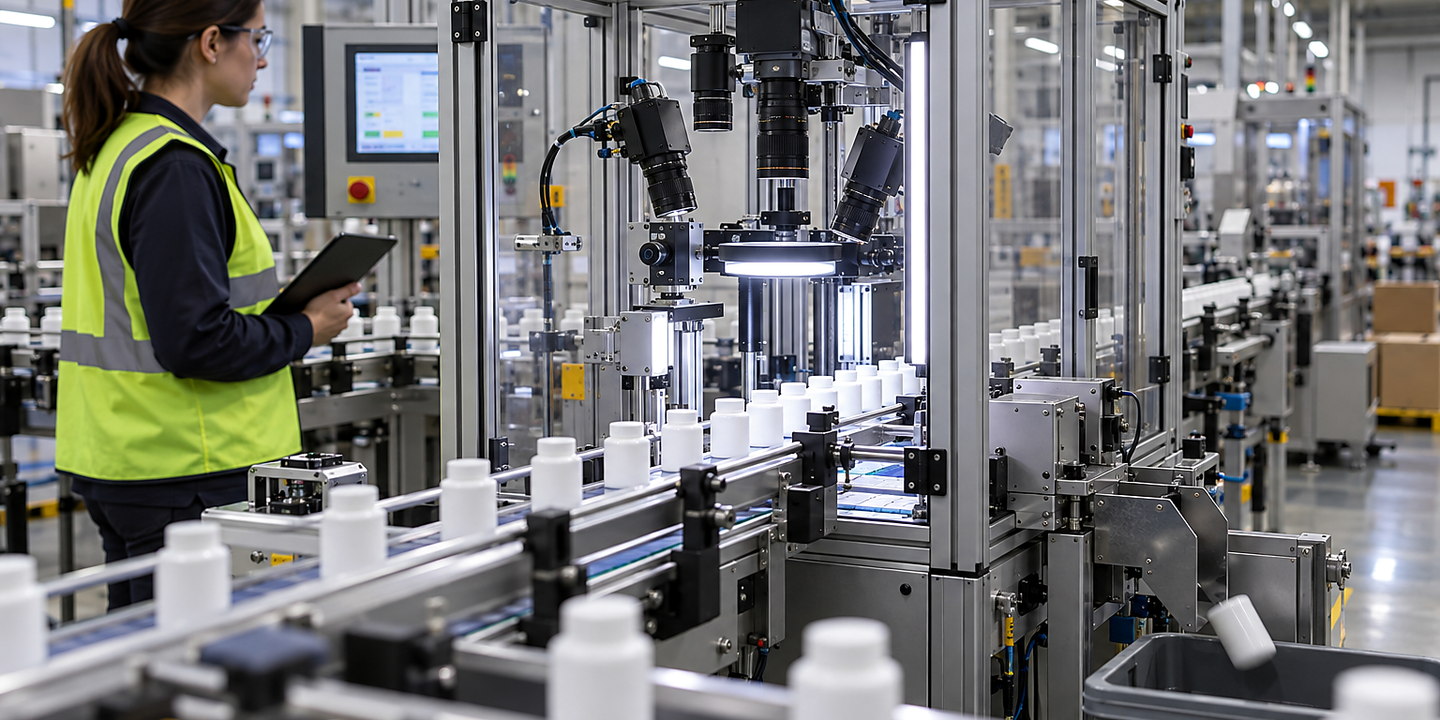
Plan documentation, training, spares, maintenance and change control for bottle checkweighers.
Illustrative bottling-line scene.
Reliable support for bottle checkweighers starts with safe access, clear diagnostics, controlled settings, maintainable parts and information your team can use.
Your support plan should match the people responsible for in-line weight checking of filled bottles, the production risk and the response your site needs.
Plan bottle checkweighers around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence. Plan the information, access and response needed to keep your operation running safely and consistently.
Discuss your application

Provide current operating, maintenance and safety information for Bottle Checkweighers, plus settings, software backups, training and any outstanding actions.
Set inspection, cleaning, calibration where applicable and wear-part tasks around reject device, removal confirmation and reject-bin state.
Give the people responsible for in-line weight checking of filled bottles clear fault information, safe diagnostic access, escalation routes and a controlled restart.
Review new products, parts, software, materials or rates before altering settings that affect test packs, challenge method, records and production response.
Record pack format, line rate, spacing, transfers, vibration and the current condition of filled bottles, closures and bottle-to-bottle tare variation.
Use approved test packs and procedures; do not defeat guarding, rejection or reject-bin monitoring during diagnosis.
Confirm the next accepted pack, physical rejection and required line response, then retain the test and action record.
A new variant or higher rate can alter filled bottles, closures and bottle-to-bottle tare variation, smallest meaningful weight difference and acceptance window, pack dimensions, stability and conveyor presentation, line speed, spacing, vibration and transfer conditions, reject device, removal confirmation and reject-bin state, and test packs, challenge method, records and production response. Record the change, assess consequences and repeat the relevant trial or validation rather than assuming the previous result transfers.