Bottle Checkweighers FAQs
Straight answers to common questions about bottle checkweighers, including suitable applications, limitations and what to send us.
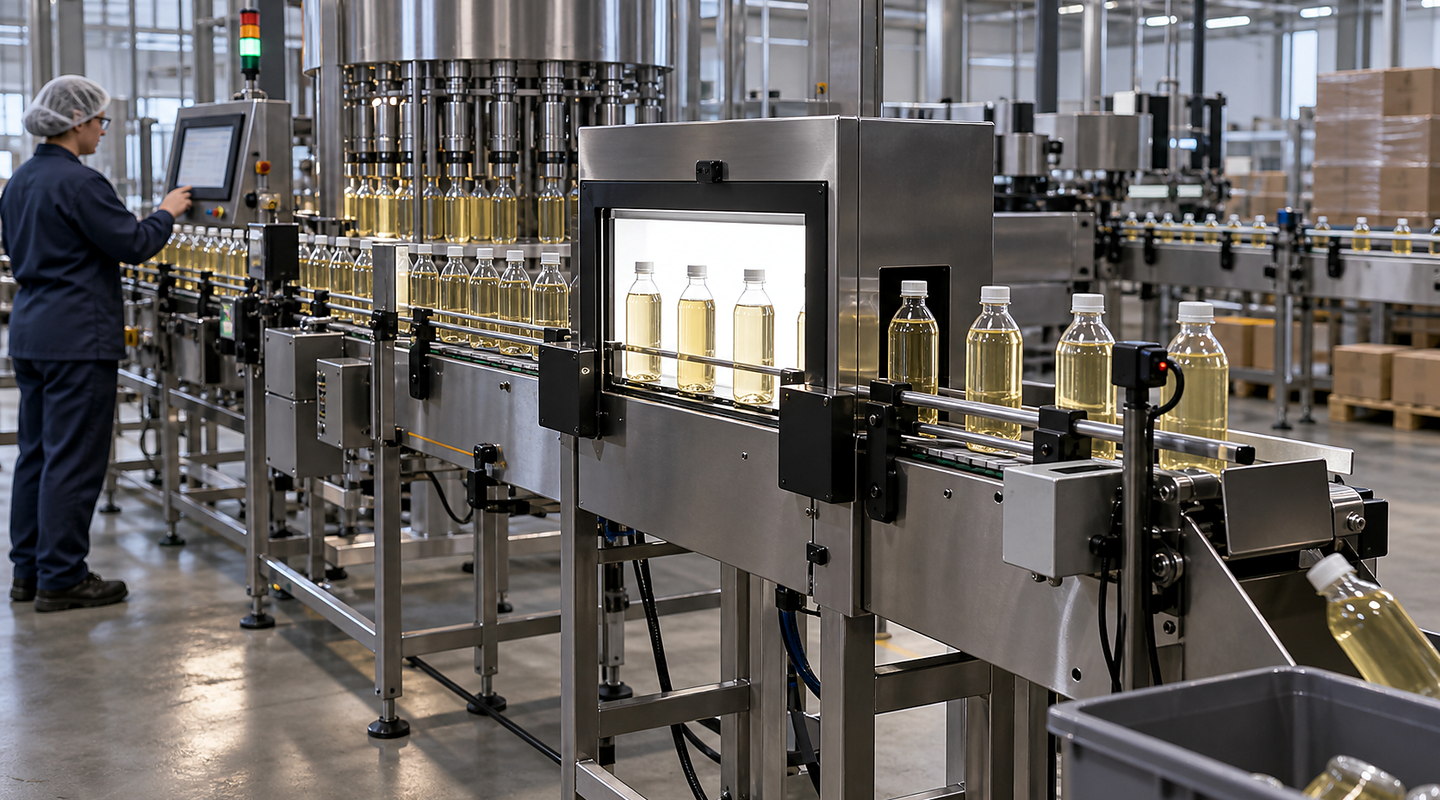
Illustrative bottling-line scene.
Useful answers about bottle checkweighers depend on your application, operating range and the results you need.
Your final bottle checkweighers scope must also account for reject device, removal confirmation and reject-bin state, test packs, challenge method, records and production response, current regulations and the conditions at your site.
Get practical answers for your application — Bottle Checkweighers
Plan bottle checkweighers around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence. The answers below explain suitable applications for Bottle Checkweighers, what information helps and what still needs an application-specific check.
Discuss your application
Practical answers about bottle checkweighers
What should we specify for checkweighing our bottles at line speed?
For bottle checkweighers, measure normal product and tare variation, define the smallest meaningful weight difference and trial representative packs at the intended speed and transfer conditions. Challenge the reject device and prove physical removal and confirmation, not only the reject signal.
How should a project for bottle checkweighers begin?
Define the real duty and collect representative samples or observations. Record filled bottles, closures and bottle-to-bottle tare variation, smallest meaningful weight difference and acceptance window, and pack dimensions, stability and conveyor presentation before choosing an approach.
Can you quote bottle checkweighers from a short description?
An early budget range may be possible, but a reliable scope for in-line weight checking of filled bottles needs the product or part range, line connections, site conditions and your requirements for test packs, challenge method, records and production response.
What information should we send about bottle checkweighers?
Share authorised drawings or photographs, representative examples from in-line weight checking of filled bottles, current process data, your production pattern, available services, space and known safety or quality requirements.
How will performance be checked?
Use an agreed trial covering normal, difficult and fault conditions for in-line weight checking of filled bottles. Judge the complete system using the agreed requirements for test packs, challenge method, records and production response, not a catalogue maximum.
What are the main limitations?
A checkweigher can only detect a fault that creates a meaningful weight difference. Normal product and packaging variation must be understood before setting an acceptance window. A reject signal is not proof that the failed pack was physically removed and confirmed.
What alternatives should be considered for in-line weight checking of filled bottles?
Compare static or sample weighing where every pack need not be checked in line with upstream process control where the fault is better prevented or measured at source. For Bottle Checkweighers, the practical option may be simpler than the most automated one.
Can the proposed solution guarantee regulatory compliance?
No solution can guarantee compliance on its own. Applicable law, current standards, risk assessment, validation and conformity responsibilities must be addressed for your complete application.
Who will handle my enquiry?
Oxford Vision Systems will receive enquiries from bottlecheckweighers.co.uk. Call 01865 416657 or email sales@oxfordvisionsystems.co.uk to speak with the team directly.
Questions to resolve before specification
Bottle stability, liquid movement, closure mass and transfer geometry—not generic pack weighing. The final decision should use representative evidence from the intended production duty.
Can a bottle checkweigher detect a missing cap?
Only when the missing-cap mass is reliably outside normal fill, bottle, label and closure variation. Representative trials are needed before suitability can be confirmed.
Does liquid movement affect dynamic weighing?
product movement and unsettled transfers can disturb the weighing cycle. The size of the effect must be established with representative test data.
What bottle samples should we send?
A useful assessment set includes normal extremes, supplier and closure variants, under/overfill examples and the tallest or least stable formats.
How should rejected bottles be confirmed?
The project should prove physical removal and the required response to a failed or full reject system. The appropriate confirmation method depends on the line and reject arrangement.